Get an estimate

What Is Flip Chip Packaging and How Does It Work?

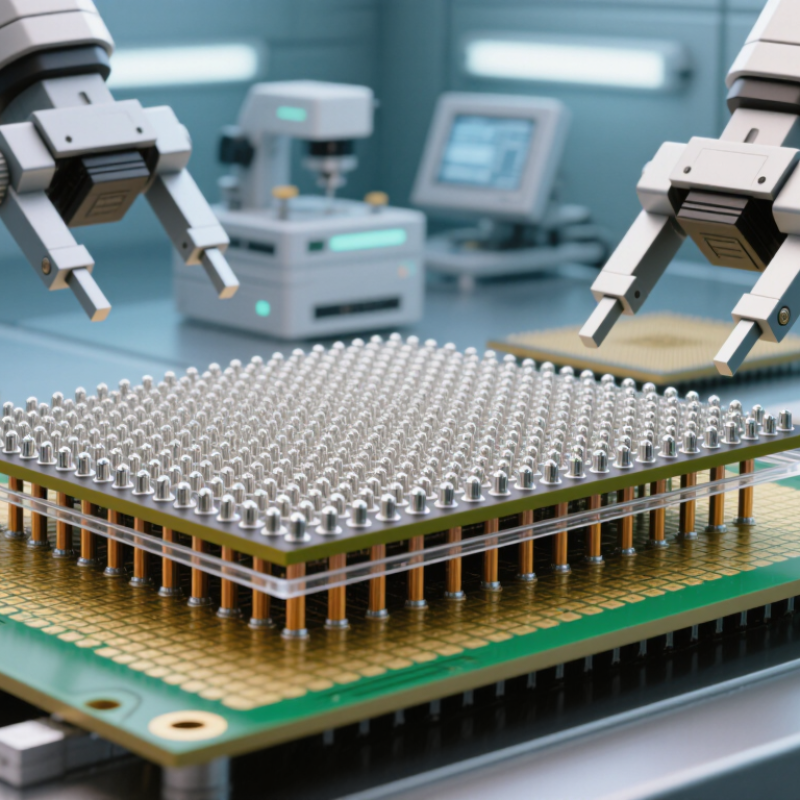
Flip Chip Packaging places a semiconductor die face down on a substrate. Tiny solder bumps or copper pillars create direct electrical and mechanical connections. Unlike traditional wire bonding, this approach shortens the signal path. It can also improve electrical performance, thermal transfer, and package density. The process begins with bump formation and wafer testing. The die is then aligned over matching substrate pads. Precision matters. A small placement error can weaken hundreds of connections.

John H. Lau, a widely recognized semiconductor packaging expert, has stated, “Flip chip technology is a key enabling technology for high-performance electronic products.” His view reflects the technology’s role in processors, graphics devices, networking hardware, and advanced sensors. During assembly, controlled heating reflows the solder joints. Underfill material often fills the narrow gap beneath the die. It reduces stress caused by different material expansion rates. Inspection may include X-ray imaging, electrical testing, and thermal evaluation.

The method is powerful, but it is not automatically better in every design. Warpage, voids, contamination, and uneven underfill can reduce reliability. Engineers must balance cost, substrate choice, heat removal, and repair difficulty. That balance deserves closer attention. This article explains how Flip Chip Packaging works, from bump creation to final testing. It also examines common materials, manufacturing stages, advantages, limitations, and practical reliability concerns. Some details vary by application. A mobile processor, automotive controller, and high-power module may require very different package structures. Understanding those differences prevents overly simple conclusions. Even a well-designed package can fail when production control is weak.
What Is Flip Chip Packaging and How Does It Work?

Flip Chip Packaging: Direct Die-to-Substrate Interconnection with 100–2,000+ I/Os

Flip chip packaging connects a silicon die directly to a substrate through solder bumps or copper pillars. The die is flipped, so its active surface faces the substrate. This short path supports dense electrical routing and reduces package resistance. In advanced designs, 100 to more than 2,000 I/Os can fit beneath one die. That density matters for processors, memory devices, and high-speed signal systems.

During assembly, engineers place bumps on matching substrate pads with precise alignment. Controlled heating forms reliable joints, while underfill spreads stress beneath the die. Inspection commonly checks bump height, voids, alignment, and connection continuity. From practical failure analysis, tiny alignment errors can become expensive electrical defects. Heat also travels through a shorter route, but thermal limits still require careful design. A compact interconnect does not automatically solve cooling problems.

The substrate must manage power delivery, signal integrity, and mechanical expansion at once. Design teams simulate impedance, current density, warpage, and thermal cycling before production. They also test samples through temperature changes and repeated operating loads. One limitation deserves attention: repair is difficult after the die is attached. Yield can suffer when thousands of joints must perform consistently. The design is powerful, but not forgiving. Unexpected warpage or uneven underfill can still undermine an otherwise advanced package.
Bump Formation: Solder or Copper Pillars at 80–300 µm Pitch

What Is Flip Chip Packaging and How Does It Work?

Bump Formation: Solder or Copper Pillars at 80–300 µm Pitch

Flip chip packaging connects a die directly to its substrate through an array of microscopic bumps. At an 80–300 µm pitch, each connection must align within a narrow process window. Solder bumps are formed by depositing solder, then using reflow to create rounded joints. Copper pillars use electroplated copper with a thin solder cap. They provide better stand-off control and support finer spacing. The choice depends on current density, thermal cycling, die size, and assembly cost.

During production reviews, engineers inspect bump height, diameter, coplanarity, and voiding. A small height variation can leave one corner electrically open. Excess solder may bridge neighboring bumps. According to Yole Group’s 2024 advanced packaging market analysis, advanced packaging demand is expanding as high-performance computing requires higher interconnect density. SEMI also reported continued growth in advanced packaging materials investment through 2028. These figures show market momentum, but they do not remove practical yield problems. Pitch alone is not a quality guarantee.

Tips: Match the bump design to the substrate finish and warpage profile. Verify UBM adhesion before full-volume plating. Use X-ray inspection for hidden joints, and cross-sections for process learning. Copper pillars can improve geometry, but they add plating control requirements. Solder remains simpler in many applications. The “best” option is rarely universal. Temperature profiles also deserve repeated review. A technically sound design may still fail after moisture exposure, uneven pressure, or rushed inspection.

What Is Flip Chip Packaging and How Does It Work? — Bump Formation: Solder or Copper Pillars at 80–300 µm Pitch

Representative bump-formation parameters used in fine-pitch flip-chip interconnects. Actual values depend on die size, electrical requirements, assembly equipment, substrate design, and reliability targets.

Design or Process Dimension Solder Bumps Copper Pillars Why It Matters in Flip-Chip Packaging
Typical bump pitch 80–300 µm 80–300 µm Pitch is the center-to-center distance between adjacent bumps. Smaller pitch increases interconnect density but tightens lithography, placement, and inspection tolerances.
Primary conductive structure Nearly the entire bump is formed from a solder alloy. A plated copper post carries most of the current, usually with a smaller solder cap on top. Copper pillars provide a more rigid and dimensionally controlled stand-off, while solder bumps provide the reflowed metallurgical joint.
Common solder composition Lead-free tin-based alloys, often using tin with silver and copper additions. A lead-free tin-based solder cap is commonly used over the copper pillar. Lead-free alloys are widely used to meet environmental and regulatory requirements; alloy selection affects melting temperature, fatigue life, and process window.
Approximate bump or pillar diameter 40–150 µm 20–100 µm copper post Diameter must leave sufficient spacing for solder bridging prevention, routing, underfill flow, and electrical isolation.
Typical total interconnect height 40–120 µm 30–100 µm Interconnect height influences substrate clearance, underfill volume, warpage sensitivity, and thermo-mechanical stress.
Approximate solder volume About 20–100 µm equivalent solder height About 5–40 µm solder-cap thickness Lower solder volume in a copper-pillar structure helps limit solder collapse and supports finer-pitch assembly.
Bump formation method Under-bump metallization is prepared, solder is deposited by methods such as electroplating or printing, and the deposit is reflowed into a controlled bump. A resist mold defines the feature, copper is electroplated to form the pillar, and a solder cap is deposited and reflowed or shaped. Photoresist thickness, plating uniformity, seed-layer quality, and bump coplanarity directly affect assembly yield.
Typical reflow peak for lead-free assembly Approximately 235–250 °C Approximately 235–250 °C for the solder cap The exact thermal profile depends on alloy chemistry and package materials. Excessive peak temperature can damage low-k dielectrics or increase warpage.
Melting and joining behavior The solder bump melts and wets both the die-side and substrate-side metallization during reflow. The solder cap melts and forms the joint, while the copper post remains substantially solid during normal solder reflow. The solid copper post limits vertical collapse and helps maintain a more predictable gap between the die and substrate.
Electrical resistance Low resistance, with the value influenced by solder volume, bump geometry, alloy resistivity, and joint quality. Generally lower resistance for the same interconnect size because copper has much lower electrical resistivity than solder. Lower interconnect resistance can reduce voltage drop and resistive power loss, particularly in high-current power and ground connections.
Current-carrying capability Suitable for signal, power, and ground connections when bump size and thermal limits are properly designed. Well suited to high-current paths because the copper post provides a larger conductive cross-section. Current density must be checked for electromigration, joule heating, and local thermal gradients.
Self-alignment during reflow Molten solder surface tension can provide useful self-alignment between the die and substrate. The solder cap provides some self-alignment, but the rigid copper post makes placement accuracy and coplanarity especially important. Self-alignment does not correct major placement errors, excessive warpage, open joints, or solder bridging.
Stand-off control More sensitive to solder volume, pad geometry, collapse, and reflow conditions. Typically better controlled because the copper post defines most of the interconnect height. Controlled stand-off improves underfill access and reduces variation in thermo-mechanical stress across the die.
Thermal and mechanical behavior Solder is relatively compliant and can absorb some differential expansion, but it is more vulnerable to creep and fatigue at elevated temperature. Copper provides higher stiffness and conductivity, while the solder cap and underfill accommodate part of the expansion mismatch. Package design must balance stiffness, compliance, die stress, substrate warpage, and thermal cycling reliability.
Underfill requirement Commonly used to distribute stress and improve thermal-cycle reliability, especially for larger dies and organic substrates. Also commonly used; the controlled pillar height can improve underfill flow and gap uniformity. Underfill selection depends on gap height, filler size, viscosity, cure temperature, moisture sensitivity, and reliability requirements.
Common process risks Solder bridging, voids, non-wetting, insufficient collapse, excessive collapse, and intermetallic growth. Pillar height variation, pillar tilt, copper plating non-uniformity, solder-cap defects, bridging, and coplanarity errors. Inspection may include optical measurement, X-ray imaging, cross-section analysis, electrical testing, and thermal-cycle qualification.
Best-fit application tendency General-purpose flip-chip interconnects where a comparatively simple solder-based joint and reflow process are appropriate. Fine-pitch, high-I/O, high-current, or thermally demanding applications requiring controlled stand-off and reduced solder volume. The preferred structure is determined by pitch, current density, die size, substrate capability, cost, assembly yield, and reliability objectives.
Engineering note: The ranges above are representative industry design values rather than universal specifications. At the lower end of the 80–300 µm pitch range, process capability is strongly affected by bump coplanarity, wafer-level lithography, substrate registration, die warpage, flux control, and inspection resolution.

Flip-Chip Assembly: Die Flipping, Alignment, Reflow, and Underfill

What Is Flip Chip Packaging and How Does It Work?

Flip-chip assembly connects a silicon die directly to a substrate through tiny solder bumps. The die is flipped, exposing its active surface downward. Unlike wire bonding, this path shortens electrical connections and improves signal integrity. Yole Group’s 2023 Advanced Packaging study estimated the market at $44.3 billion in 2022, with growth toward $78.3 billion by 2028.

Die flipping requires controlled handling. A placement tool aligns each bump with its matching substrate pad, often within micrometer-level tolerance. Cameras inspect fiducial marks before contact. Even slight misalignment can create opens, bridges, or uneven stress. It sounds simple. It is not.

During reflow, the solder bumps melt and form mechanical and electrical joints. Temperature profiles must rise evenly, avoid excessive oxidation, and limit warpage. After cooling, liquid underfill flows beneath the die by capillary action. It fills air gaps and spreads thermal-mechanical stress across the joint field. Void control remains difficult, especially beneath large dies. SEMI reported $67.5 billion in global semiconductor materials sales for 2023, showing the scale of the wider manufacturing ecosystem. Yet material volume does not guarantee assembly quality. Engineers still need cross-section analysis, thermal cycling, and electrical testing. Some failures appear only after long operation.

Electrical and Thermal Benefits: Shorter Paths and Up to 10× Better Heat Transfer

Flip chip packaging places a silicon die face down, connecting its pads directly to the substrate. Tiny solder bumps replace longer wire-bond routes. This geometry reduces electrical distance, parasitic inductance, and signal delay. IEEE packaging studies commonly report shorter interconnects as a key advantage for high-speed power and data transmission.

Thermal performance can improve sharply. Heat travels through many direct bump connections instead of moving around the die edge. Under matched materials, controlled pressure, and suitable heat spreaders, industry studies report up to 10× higher heat-transfer capability than some conventional wire-bond packages. The result can be lower junction temperature and greater power density. Real gains vary.

The 2023 IPC Advanced Packaging Technology Roadmap links advanced interconnect density with rising thermal-management demands. JEDEC thermal-test methods also stress careful measurement, because laboratory values can differ from assembled-system performance. That distinction matters. A package may show excellent thermal resistance on paper, yet perform less effectively after board mounting, aging, or uneven solder joints.

In practice, engineers inspect bump pitch, substrate thickness, underfill behavior, and cooling-interface flatness. Shorter paths help electrically, but they do not solve every reliability problem. Warpage remains a concern. So does thermal expansion mismatch. Flip chip is powerful, though not automatically superior in every design.

Industry Applications: CPUs, GPUs, HBM, RF Chips, and 2.5D/3D Packages

Flip chip packaging mounts a semiconductor die face down on a substrate or interposer. Tiny solder bumps connect the die directly to external circuits. This short path reduces electrical resistance, signal delay, and package size. During assembly, the die is aligned, bonded, and protected with underfill material. Underfill helps distribute mechanical stress beneath the chip. That sounds simple, but alignment tolerances are extremely tight.

CPUs use flip chip structures to support dense power delivery and fast data movement. GPUs need even more connections for parallel computing and high-speed memory access. HBM places memory dies in vertical stacks, often beside a processor on a 2.5D interposer. This arrangement creates wide data paths with impressive bandwidth. Spacing matters. RF chips also benefit from short connections, which can reduce parasitic effects and signal loss. However, RF performance depends heavily on substrate design, shielding, and thermal control.

In 2.5D packages, several dies sit side by side on an interposer. In 3D packages, dies stack vertically through fine-pitch connections. These layouts save space but increase manufacturing difficulty. Heat must escape through crowded layers. Thermal expansion can also strain solder bumps and underfill. A perfect layout is rarely realistic. Engineers balance bandwidth, yield, cost, inspection, and reliability. Small voids or warpage may remain difficult to detect, especially when package density keeps increasing.

Representative Interconnect Pitch by Flip Chip and Advanced Package Application

Flip chip packaging connects a die to a substrate, package or interposer through an array of conductive bumps, allowing short electrical paths and high I/O density. The values shown are representative industry-level pitch values in micrometers: conventional CPU, GPU and RF flip-chip assemblies generally use larger pitches, while HBM, 2.5D interposers and 3D hybrid-bonding structures use progressively finer interconnects. Actual values vary by process generation, package design and electrical requirements.