Get an estimate

FR209E Type Coupler Body Suppliers and Specifications

FR209E Type Coupler Body suppliers serve a demanding rail equipment market. Their products must support reliable coupling, controlled force transfer, and long service life. The body is more than a cast or forged housing. It is a load-bearing component that works through vibration, impact, weather, and repeated maintenance cycles.

Railway equipment engineer Daniel Mercer explains, “A coupler body should be judged by verified performance, not by appearance alone.” This practical view matters when comparing suppliers and specifications. Buyers should review material grades, heat-treatment records, dimensional tolerances, machining accuracy, and inspection procedures. Traceability is equally important. Each production batch should connect clearly to test reports and quality records.

Look closely at the details.

A dependable supplier can provide drawings, reference standards, surface-finish data, and compatibility information. The FR209E design may require precise interfaces around the shank, knuckle area, mounting surfaces, and locking mechanism. Small dimensional errors can create alignment problems during installation. They may also increase wear in connected parts.

Supplier experience deserves careful attention. Ask whether the manufacturer has produced comparable coupler bodies for heavy rail, freight, or industrial applications. Factory audits, sample inspections, and non-destructive testing can reveal weaknesses that brochures hide. Still, specifications alone do not guarantee field performance. Installation conditions, maintenance quality, and operating loads also influence service life.

One uncertainty remains.

Public information about some FR209E configurations may vary between suppliers. Buyers should confirm the exact drawing revision, material requirement, inspection scope, and delivery documentation before ordering. This introduction examines those points closely, while recognizing that a polished specification sheet is not always the complete engineering story.
FR209E Type Coupler Body Suppliers and Specifications

FR209E Type Coupler Body: Definition and Core Functions

The FR209E type coupler body is the main structural shell of a railway coupler assembly. It holds internal parts and transfers pulling and pushing forces between connected vehicles. During operation, the body absorbs repeated loads, vibration, and occasional impact energy. Its job is simple. It must remain strong under changing conditions. A properly made body also keeps connected components aligned during service.

Specifications usually cover material grade, casting or forging method, dimensions, weight, and surface condition. Engineers check the coupler pocket, locking areas, mounting faces, and load-bearing edges carefully. These locations influence fit, movement, and long-term durability. Material selection should balance strength, toughness, wear resistance, and resistance to cracking. Critical surfaces may require controlled machining and defined dimensional tolerances. The designation alone does not confirm every measurement. Approved drawings and current technical standards remain necessary.

A reliable supplier should provide inspection records, material certificates, dimensional reports, and traceable production information. Receiving teams can measure mounting holes, contact surfaces, and key clearances before installation. Look for cracks, sharp casting defects, distortion, or uneven machining marks. Visual checks matter. However, visual inspection cannot reveal every internal flaw. Non-destructive testing may be appropriate for highly stressed areas. One practical mistake is assuming that similar coupler bodies are interchangeable. They may look alike, yet differ in geometry or load requirements. Verification prevents that costly assumption.
Design Features and Technical Specifications of the FR209E Coupler Body

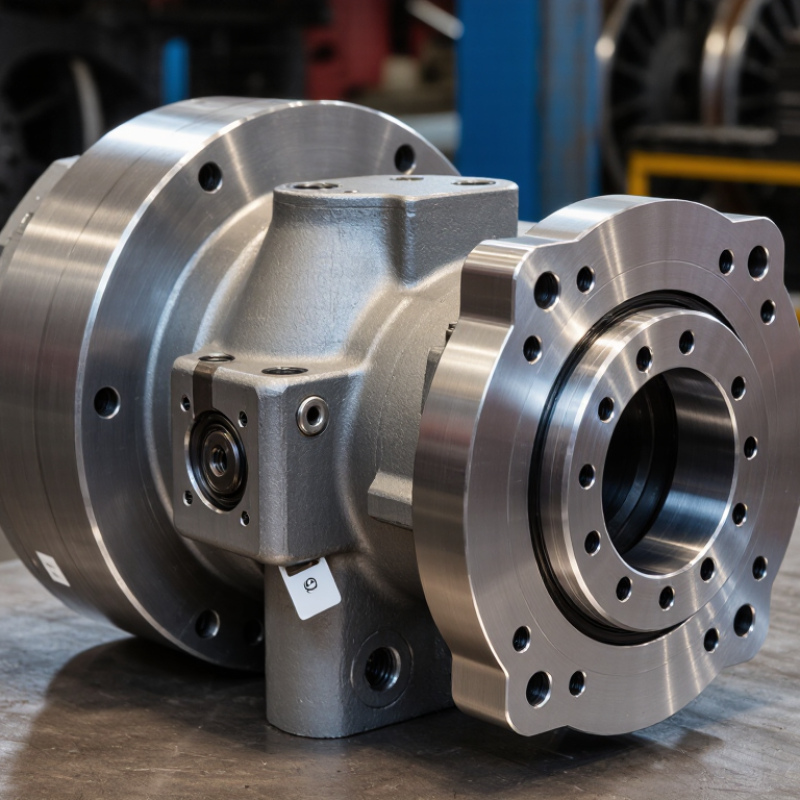
The FR209E coupler body is designed to transfer traction and buff loads through the shank, pivot area, and knuckle pocket. Its geometry must maintain alignment under repeated impact. A supplier should provide material grade, casting or forging method, heat-treatment records, and dimensional tolerances. These details matter more than a polished catalog image.

Technical verification should cover shank length, mounting-hole diameter, pocket width, body mass, and allowable wear limits. Ultrasonic inspection can reveal internal discontinuities that visual checks may miss. The UNIFE World Rail Market Study 2024 projects about 3% average annual growth in the global rail market from 2023 to 2027. Higher fleet activity may increase demand for dependable replacement bodies. It also makes traceability more important.

Not every drawing is complete.

Procurement teams should compare supplier data with the applicable railway standard and vehicle interface requirements. Tensile and compression testing should represent actual service loads, not only laboratory ideals. Surface protection, machining accuracy, and hardness consistency deserve attention around the pivot and knuckle pocket. A small mismatch can create uneven contact, noise, or accelerated wear. The specification should also state inspection frequency, repair limits, and batch identification. Some technical sheets remain vague about fatigue testing. That gap deserves written clarification before approval.

Material Selection and Manufacturing Requirements

For FR209E type coupler body suppliers, material selection should begin with the service environment, not a catalog number. The body may face impact, vibration, moisture, and repeated assembly loads. Carbon steel is often practical for strength and machinability. Low-alloy steel can offer better fatigue resistance when loads are severe. Stainless steel deserves attention where corrosion control outweighs cost. Do not assume “equivalent” means identical. The final choice should match the approved drawing, temperature range, hardness limits, and required mechanical tests.

A qualified supplier should provide heat numbers, chemical analysis, tensile results, and traceable inspection records. This evidence matters more than polished product photos. For a forged or machined body, process control begins with sound billet preparation and controlled forming. Machining allowances must protect critical bores, threads, shoulders, and sealing faces. Sharp transitions need review. They can concentrate stress. Non-destructive testing may be necessary after machining, especially around high-load sections. However, inspection scope should follow the engineering specification, not habit.

Suppliers should confirm dimensional tolerances with calibrated gauges and record actual measurements. A useful first-article report shows bore diameter, center distance, wall thickness, and surface condition. I have seen small burrs disrupt assembly even when major dimensions passed inspection. That detail is easy to miss. Packaging also matters. Oil protection, separators, and capped openings can prevent damage during storage and transport. One practical weakness remains: buyers sometimes request material certificates after production. That timing limits corrective action. Specify documentation, testing, and acceptance criteria before the purchase order is released.

FR209E Type Coupler Body Suppliers and Specifications - Material Selection and Manufacturing Requirements
Category Specification Item Requirement Inspection or Reference
Product Identification and Service Function
Product Component designation FR209E type railway coupler body intended for freight-car or locomotive coupler assemblies. Approved product drawing and purchase specification
Function Load-bearing application The body shall transmit longitudinal tensile and compressive forces through the coupler assembly without cracking, excessive permanent deformation, or loss of compatibility with the mating components. Design review and final inspection
Configuration Basic construction One-piece precision steel casting with integral front, shank, follower, carrier, and draft-system interface features as defined by the approved FR209E drawing. Dimensional inspection
Material Selection
Base material Cast steel grade Low-alloy cast steel suitable for railway coupler service, manufactured to AAR M-211 requirements or an approved equivalent material specification. Material certificate and heat-lot records
Chemical composition Typical control limits Typical maximum limits are carbon 0.35%, manganese 1.20%, silicon 0.80%, phosphorus 0.040%, and sulfur 0.040%. The governing drawing or material standard shall take precedence. Heat analysis by optical emission spectroscopy
Mechanical properties Minimum values Typical minimum requirements for a coupler-grade cast steel are tensile strength 690 MPa, yield strength 485 MPa, elongation 18%, and reduction of area 35%, unless a different approved grade is specified. Tensile test from each qualified heat-treatment lot
Heat treatment Condition Normalize and temper, or use another approved heat-treatment cycle capable of producing uniform mechanical properties throughout the casting. Furnace chart, batch record, and hardness survey
Hardness Typical control range Approximately 241–311 HBW after heat treatment, subject to the approved material grade and drawing requirements. Hardness variation within one casting shall be controlled and documented. Brinell hardness testing in representative locations
Material cleanliness Inclusions and internal quality Steel shall be free from harmful oxide films, slag inclusions, shrinkage cavities, hot tears, and other discontinuities that could reduce fatigue strength or load-carrying capacity. Metallurgical review and NDT reports
Casting and Manufacturing Requirements
Pattern and tooling Pattern control Pattern dimensions shall include approved casting allowances for shrinkage, machining, draft, and distortion. Pattern revision status shall match the released FR209E drawing. Pattern inspection and revision control
Melting Process control Use controlled melting practice with recorded charge materials, furnace identification, tapping temperature, deoxidation practice, and heat number. Foundry process record
Gating and risering Solidification control Gating and risering shall promote directional solidification and minimize shrinkage in the shank, throat, front face, and draft-interface regions. Approved casting simulation or process qualification
Fettling Removal of casting appendages Risers, gates, flash, fins, and parting-line projections shall be removed without reducing the minimum design section or creating sharp stress raisers. Visual and dimensional inspection
Weld repair Repair restrictions Weld repair shall not be permitted in critical load-bearing areas unless specifically authorized by the purchaser. Any approved repair shall use a qualified welding procedure and qualified welders. Welding procedure, welder qualification, and repair map
Machining Machined interfaces Machined surfaces shall be produced from stable heat-treated castings. Critical holes, bearing faces, pivot areas, and draft-system interfaces shall be located from the drawing datums. CMM or calibrated gauge inspection
Dimensional and Surface Requirements
Overall dimensions Geometry control Overall length, height, width, coupler contour, shank profile, and interface locations shall conform to the approved FR209E drawing. Drawing dimensions take precedence over catalogue values. First-article and final dimensional report
Critical tolerances Datum-based features Critical mating dimensions, hole locations, pivot features, and draft-gear interfaces shall be controlled by individual drawing tolerances; general casting tolerances shall not be applied to these features. CMM, functional gauges, or calibrated fixtures
Surface condition As-cast finish After shot blasting or approved cleaning, the casting shall be free from adhering sand, scale, fins, cracks, folds, laps, and visible open defects. 100% visual inspection
Surface roughness Machined areas Machined surface roughness shall comply with the individual drawing requirement. Unspecified as-cast areas shall be uniform and free from loose scale or unstable surface material. Surface comparator or calibrated roughness tester
Non-Destructive Testing and Acceptance
Magnetic particle testing Surface discontinuities Perform magnetic particle inspection on critical accessible surfaces after final cleaning and before protective coating. Linear indications, cracks, and crack-like indications are unacceptable. ASTM E1444/E1444M or approved equivalent
Ultrasonic testing Internal discontinuities Ultrasonic inspection shall cover critical load-bearing sections identified by the drawing or quality plan. Rejectable indications shall be evaluated against the approved acceptance level. ASTM E114 or approved equivalent
Radiographic testing Volumetric inspection Radiographic examination may be required for process qualification, suspect areas, or critical sections where internal shrinkage and inclusions cannot be adequately assessed by other methods. ASTM E446/E186 or approved equivalent
Proof or functional testing Assembly compatibility Where required by the governing railway specification, the completed body shall pass dimensional fit checks and proof-load or functional tests without cracking, permanent deformation, or interference. Approved test procedure and inspection report
Traceability, Documentation, and Delivery
Traceability Identification marking Each casting shall be traceable to the steel heat, casting batch, heat-treatment lot, inspection status, and production date through permanent marking or an approved traceability system. Marking verification and batch records
Inspection documentation Required records Supply the material certificate, chemical analysis, mechanical test results, heat-treatment chart, hardness results, dimensional report, NDT reports, and nonconformance disposition where applicable. Document review before shipment
Calibration Measurement equipment All gauges, measuring equipment, hardness testers, and NDT instruments used for acceptance shall have valid calibration traceable to recognized national or international standards. Calibration certificates
Protective treatment Storage protection After final inspection, apply a temporary rust-preventive treatment compatible with the specified coating or assembly process. Protect machined and mating surfaces during transport. Visual inspection and packaging review
Packaging Handling and shipment Use supports that prevent impact damage and distortion. Separate castings to avoid metal-to-metal damage and keep identification marks legible during transport and storage. Pre-shipment inspection
Technical note: FR209E-specific dimensions, load ratings, acceptance limits, and any railway-operator requirements shall be taken from the latest approved drawing and governing procurement specification. Where a value is identified as typical, the released design and applicable material standard shall take precedence.

How to Evaluate and Select Reliable FR209E Coupler Body Suppliers

FR209E Type Coupler Body Suppliers and Specifications

Selecting a reliable FR209E coupler body supplier requires more than comparing unit prices. Review material certificates, dimensional drawings, heat-treatment records, and inspection results before approval. The body should match specified tolerances, load requirements, surface protection, and assembly conditions. Ask for traceability from raw steel to final inspection.

Supplier resilience also matters. McKinsey’s global operations survey reported that 93% of supply-chain leaders planned to improve resilience after major disruptions. This supports checking dual-source planning, production capacity, safety stock, and realistic lead times. A supplier with clear contingency procedures may protect your project better than a cheaper supplier with limited records.

Use ISO 9001 certification as evidence, not proof. The ISO Survey reports more than one million certified organizations worldwide, but certificates do not guarantee consistent coupler quality. Request recent nonconformance data, corrective-action reports, and sample inspection sheets. Verify hardness, weld quality, hole position, and dimensional repeatability through independent testing when the application is demanding.

Ask technical questions early. Can the supplier reproduce the FR209E profile? Which measurement equipment is calibrated? How are design changes controlled? The answers reveal practical competence. One weakness remains: many evaluations overvalue paperwork and undervalue production-floor experience. A factory tour, sample approval, and small trial order can expose that gap. Documentation can look perfect. Performance may not.

Quality Standards, Inspection, and Application Considerations

FR209E Type Coupler Body Suppliers and Specifications

Quality begins with evidence, not attractive specifications. During supplier audits, experienced buyers should check heat numbers, forging records, machining reports, and final inspection photographs. Each FR209E coupler body should have traceability from raw material to shipment. That detail matters when a crack appears after repeated coupling impacts. It also exposes weak documentation.

The ISO Survey 2023 recorded more than one million ISO 9001 certificates worldwide. Certification helps, but it does not prove coupler performance. Suppliers should also demonstrate dimensional control, ultrasonic or magnetic-particle inspection, hardness results, and load-test records. Critical surfaces need clear tolerances, especially around the knuckle seat, pin bore, and mounting interfaces. A practical inspection plan should define sampling frequency, gauge calibration, rejection limits, and corrective-action timing.

Application conditions can change the specification. Freight service may demand high impact resistance, while passenger equipment can prioritize weight, noise, and maintenance access. The UNIFE World Rail Market Study 2024 valued the global rail supply market at approximately €201 billion annually for 2023–2027. That scale increases purchasing pressure, yet rushed substitutions can create interface problems. Confirm coupler geometry, operating temperature, corrosion exposure, and compatible draft gear before approval. Site trials should record alignment, wear patterns, and coupling force. Laboratory data alone is incomplete. A supplier may meet every drawing dimension and still miss a field reality. That deserves review.

Article Source: